How to Make a Longboard Deck: Step-by-Step (Without a CNC)
This post contains affiliate links. As an Amazon Associate, we earn from qualifying purchases.
To make a longboard deck, you press layered wood veneers and composite materials inside a custom two-part mold under high pressure. A professional deck, per World Industries Skateboards, must withstand 3,200 lbs at the center and 2,700 lbs at the tongue (nose/tail region). The process involves building a mold from templates, preparing a core layup (often 7-9 layers of maple veneer), and curing it under pressure for anywhere from 2 hours to 2 days, depending on your glue and press.
That load rating isn’t marketing. It’s the pass/fail line from a destructive test where a 6-inch-long 2×4 block simulates a foot. If your homemade deck can’t handle that kind of force, it’s a decoration, not a rideable board. A key part of learning how to make a longboard deck is understanding this test.
What follows is the map for how to make a longboard deck from a blank sheet of MDF to a deck you can trust at speed. We’ll walk through mold-making, the material choices that actually affect flex, and the specific glues and pressures that prevent delamination, the number one killer of DIY decks. You’ll also see where the experts disagree, because building a deck is as much art as engineering.
Key Takeaways
- Professional deck inspection requires withstanding 3,200 lbs at the center and 2,700 lbs at the tongue; a homemade deck must target these specs.
- The number one problem is delamination, traced directly to an improper glue-up, work quickly and apply enough adhesive to your veneers.
- For pressure, 175 psi or 25 tons is a good starting point; a weaker 5-ton press means much longer curing times.
- Sources disagree on curing: DIYskate.com says with proper glue and tonnage, removal can happen in 2 hours; the Fab Academy project recommends at least 8 hours under pressure; and the Australian Wood Review recommends 2 days. Check your glue manufacturer’s instructions.
- Sources disagree on how to determine deck thickness: the ETSU thesis outlines a calculated approach, while the Australian Wood Review advocates a trial-and-error method, standing on sample plywood blanks (9mm, 12mm, 15mm) placed on blocks spaced at truck width.
The Mold is Everything
Your deck’s shape, its concave, its camber, its entire personality, is born in the mold. This isn’t a suggestion. A sloppy mold translates directly to faulty bonding and predetermined breaking points. The Australian Wood Review article advocates that a two-part mold (lower and upper template) ensures the best possible functionality, while other builders, like the MIT Fab Lab project, have used a one-sided mold with a hybrid system, noting a two-sided mold may have been more effective.
Start with a full-size drawing of your deck. The Australian Wood Review article offers a reference point for a rider around 1.75m tall and 80kg: a deck 960mm long by 230mm wide. Your template needs to be longer and wider than the final deck: add 20mm to the length on both ends, and make the width at least 5mm wider than your finished board on each side. This accounts for material spring-back and trimming.
Now, build the mold itself. The most accessible method uses stacked MDF. Glue printed deck shapes onto MDF sheets, then cut and sand them to the markings. Stack and glue these profiles together to form the positive shape of your deck’s top and bottom. This creates a solid, reusable mold block. Here’s the critical, often-missed detail: when you mill the concave and camber into these stacked profiles, the radii on your two mold halves cannot be identical. The material you’re pressing between them has thickness. If you don’t account for that, the pressure won’t distribute evenly. For very tight radii, this mis-match guarantees weak spots.
Common mistake: Assuming both halves of a two-part mold can be milled with identical curves. The pressed material’s thickness changes the effective radius, leading to uneven pressure and weak bonds that fail under load.
Some builders, like the MIT Fab Lab project, use a one-sided mold (like an old longboard) with a hybrid compression/vacuum system. They note a two-sided mold may have been more effective, but for slight bends, their method worked. For a first-time build with complex concave in how to make a longboard deck, stick with the two-part approach. It’s more predictable.
The Core Layup: Veneer, Fiberglass, and Glue
This is where your deck gets its strength and soul. You’re not just gluing wood together; you’re creating a composite beam. The materials and their orientation are critical.
The classic core in industry specifications uses Canadian Maple veneer sheets 0.058” thick. For a standard 7-ply deck, you alternate the grain direction perpendicularly between layers. This cross-graining gives a skateboard its torsional stiffness. The bottom veneer is often laid longitudinal for aesthetics. The number of layers isn’t fixed; it depends on the rider’s weight and desired flex. Other builds, like the anecdotal one from Fab Academy, use 7 to 9 layers of 1.58mm thick maple with bamboo outer layers.
But a high-performance longboard isn’t just wood. The Australian Wood Review build adds composite reinforcement. Their stack-up: a 10mm thick maple core with its grain rotated 90°, topped and bottomed with 700g/m² fibreglass fabric and a 0.6mm maple veneer. The top gets a decorative veneer of smoked pear wood.
The glue is the marriage license for these materials. Use a polyurethane wood glue or a dedicated skateboard adhesive like Multibond Sk8 or PC-2365. The choice dictates your entire press schedule. DIYskate.com states that with proper tonnage, these specialized glues can set in 10 minutes or less, and you can remove decks within 2 hours. But you must check with the glue manufacturer. Other sources, like the Australian Wood Review, recommend leaving resin to harden for two full days before demolding.
| Material Layer | Typical Spec | Purpose | Source of Spec |
|---|---|---|---|
| Core Maple Veneer | 0.058” thick | Primary structural strength, cross-graining for stiffness | ETSU Thesis |
| Fibreglass Fabric | 700g/m² | Impact resistance, vibration damping, prevents delamination | Australian Wood Review |
| Decorative Top Veneer | 0.6mm maple or smoked pear wood | Aesthetics, slight additional stiffness | Australian Wood Review |
| Professional Glue | Multibond Sk8, PC-2365 | Fast cure under pressure, high ultimate strength | DIYskate.com |
Apply enough glue. This sounds basic, but DIYskate.com pins delamination, the number one construction problem, directly on an improper glue-up. Work quickly, coat evenly, and don’t starve the joint. A dry spot is a future crack.
Pressing and Curing: Where Time and Pressure Meet
You have your layered stack, glued and ready. Now you need to convert that flat sandwich into a shaped deck, and that requires serious force. The industry standard for testing uses a beam deflection gauge, but your job is to apply uniform pressure across the entire mold cavity.
How much pressure? Many factors affect this, but 175 psi or 25 tons is a good starting point. This is why a 5-ton hobby press requires the veneer to be pressed for a “longer period of time.” The pressure ensures the glue flows into every wood pore and the layers knit together without gaps.
The process is methodical:
- Prepare the mold surfaces. Apply a release agent. For a first-time use on a new mold, the Fab Academy method adds an extra sacrificial layer of wood with glue on top of each mold half. A film of plastic wrap between this layer and your actual deck prevents sticking. This is a one-time step to perfect the mold’s surface finish.
- Assemble the stack in the mold. Place your layered deck materials between the mold halves, ensuring everything is aligned.
- Apply maximum pressure. Whether you’re using a hydraulic press, a threaded rod press, or a hybrid system, crank it down until the mold halves are fully closed. The goal is to squeeze out a small, even bead of glue from all edges.
- Walk away. This is the hardest part. Curing time is the great disagreement. The academic skateboard press system design from ETSU doesn’t specify a time, focusing on the engineering. DIYskate.com says 2 hours with the right glue. The Fab Academy project says at least 8 hours under pressure. The Australian Wood Review says 2 days. Who’s right? They all are, for their specific glue, material stack, and press tonnage. Your glue manufacturer’s instructions are the final word.
- Demold and post-cure. Once you open the press, the deck will hold its shape. But the glue and wood aren’t fully dry internally. DIYskate.com advises an additional 24 hours of curing after removal before any further work. The Fab Academy is stricter: leave it untouched for complete drying for at least 5 days.
Rushing the cure is the second fastest way to ruin weeks of work. The fastest way is skipping the mold-prep and getting a bond between your deck and the mold itself. Don’t let that happen.
Shaping, Sanding, and Finishing the Deck
Out of the mold, you have a deck blank, a rough, oversized lump that vaguely resembles a longboard. Now you make it precise. This phase is about patience and progressively finer steps.
First, shape the outline. Use a band saw or jig saw to cut roughly to the shape of your template. Leave a few millimeters of extra material outside your final line. This is your margin for error during sanding.
Next, tackle the edges. A professional deck has a specific edge radius, usually between 1/8″ to 3/16″. You can achieve this with a palm router and a round-over bit, or through a lot of hand sanding. The router is faster and more consistent. The goal is a smooth, rounded edge that won’t splinter on impact.
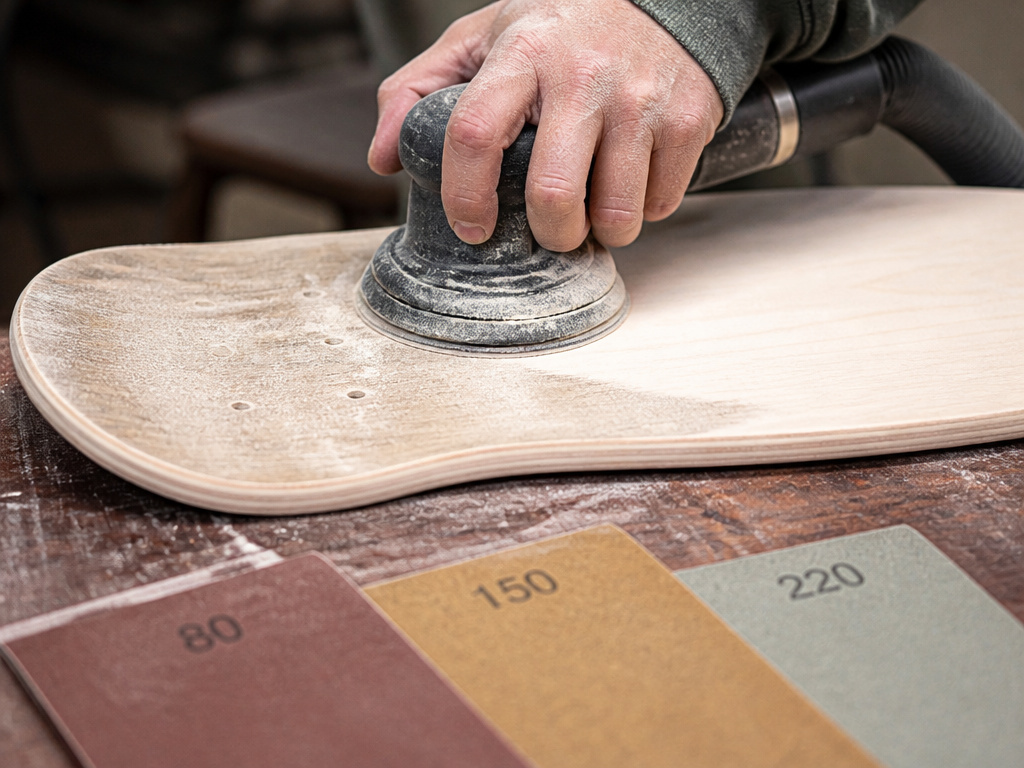
Now, sand. Start aggressive and move to fine.
- Start with 80 or 100 grit sandpaper. This removes saw marks and evens out any high spots from the mold. Use an orbital sander if you have one; it’s faster and leaves a more even surface.
- Progress through 150 grit. This begins to smooth the surface.
- Finish with 220 grit. This should leave the deck silky to the touch, with no visible scratches.
Before any finish touches the wood, you must remove all dust. Use a tack cloth, cheesecloth coated in a special wax. It picks up fine dust that a brush or rag will just push around. A dusty surface will trap particles under your sealer, creating a rough, permanent finish.
Sealing and painting come next. This is where you can add graphics to customize a longboard. The golden rule: match your paint base to your sealer base. If your sealer is water-based, use water-based paint. If it’s solvent-based, use solvent-based paint. Mixing them causes crazing, peeling, and a sticky mess that never fully dries. Apply your graphics, let them dry completely (overnight is safe), then seal everything under multiple coats of a clear polyurethane or lacquer. Each coat needs to dry fully before the next is applied. This build-up creates a durable, scratch-resistant shell.
Finally, apply grip tape. You can use full-cover black tape or cut decorative patterns. The key is to apply it smoothly, without air bubbles, and burnish the edges down firmly. A well-applied grip tape job is both functional and the final aesthetic touch when working with deck materials.
Drilling Holes and Final Assembly
Your deck is sealed, painted, and gripped. It’s a sculpture. Now you need to turn it into a vehicle. That means drilling eight precise holes for the truck mounting hardware.
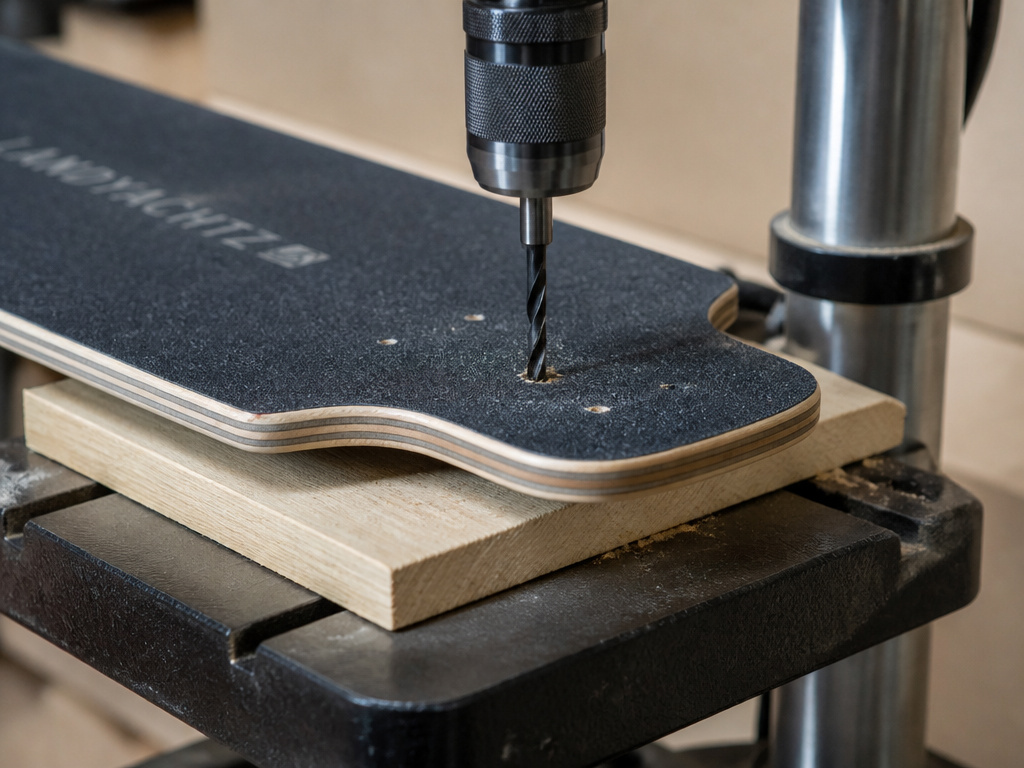
Use a drill press. A hand drill can work, but the bit must be perfectly perpendicular to the deck surface. Angled holes cause misaligned trucks, which leads to speed wobbles and uneven wear. A drill press guarantees vertical holes.
To locate the holes, you need your wheelbase, the distance between the two truck axles. You can measure this from an existing board you like, or determine it based on your deck length and riding style. Find the true centerline of your deck lengthwise. Mark your wheelbase distance centered on that line. The truck mounting holes are typically spaced in a standard pattern; you can use an old deck as a template or find the specs for your specific trucks online.
Drill slowly to prevent the veneers from splintering on the exit side. Use a scrap piece of wood underneath the deck as a backer board. Once the holes are drilled, you’re ready for complete board assembly.
Attaching the trucks is straightforward: insert the hardware through the deck, add a washer if your trucks require it, and screw into the truck baseplate. Tighten firmly, but don’t strip the threads. The final step is adding wheels and bearings. At this point, you’ve graduated from woodworker to board builder. The longboard shapes and deck flex you engineered are about to be road-tested.
How Thick Should Your Deck Be? Trial vs. Calculation
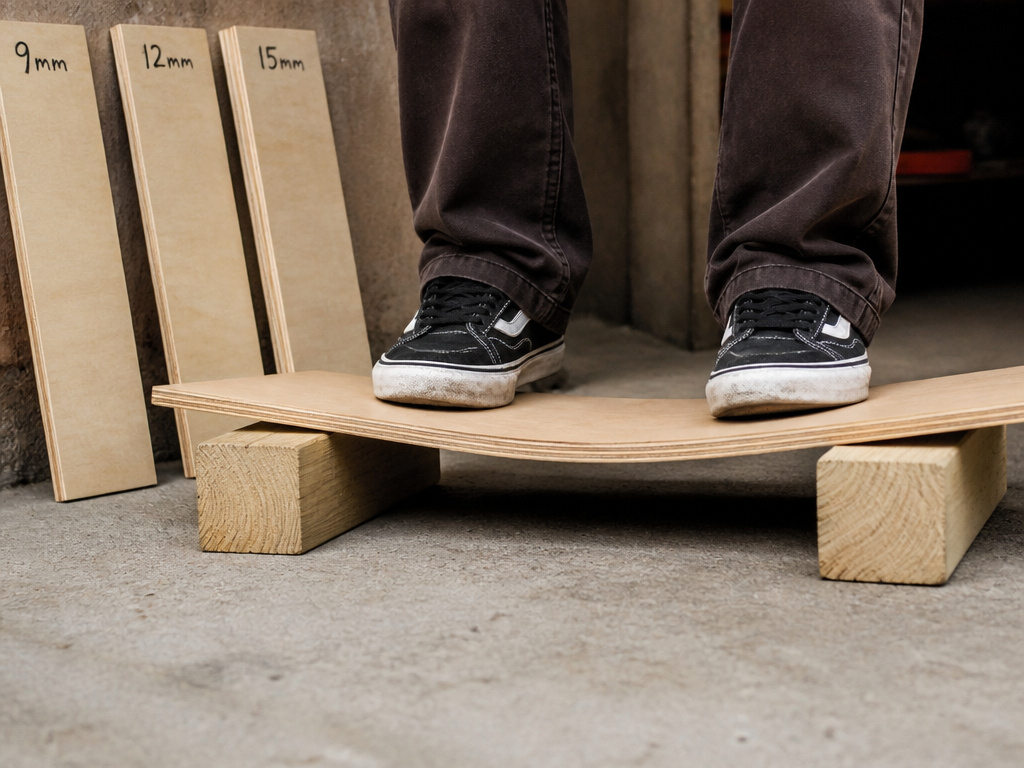
This is a fundamental question with two clashing answers from credible sources. The engineering approach, outlined in resources like the ETSU thesis, uses calculated material selection. It considers veneer count, composite reinforcement, and load requirements to derive a thickness. The other approach, championed by the Australian Wood Review, is purely empirical. The author explicitly rejected calculation after “countless attempts.”
Their method is brilliantly low-tech: get sample plywood blanks in set thicknesses (9mm, 12mm, 15mm). Place each blank on two blocks spaced at your truck width, simulating the deck’s support points. Stand on it. Bounce lightly. Feel the flex. Does it feel solid, springy, or alarmingly soft? This trial-and-error test directly correlates to how the deck will behave under your weight while riding. It accounts for your personal preference in a way a formula cannot.
For a first build, the empirical method is more forgiving. It prevents you from building a deck that’s overly stiff for cruising or dangerously flexible for downhill. Once you know the feel you like, you can reverse-engineer the thickness and ply count for your next, more calculated build.
Common Pitfalls and How to Avoid Them
Building a deck is a series of small tasks. Nail them all, and you win. Mess up one, and it can cascade. Here are the traps.
Delamination: The number one killer. It’s almost always a glue issue, not enough glue, glue that skinned over before pressing, or insufficient pressure. The fix is in the preparation: have everything ready, work fast, and use adequate tonnage.
Faulty Mold Radii: As covered, if your two mold halves don’t account for material thickness, you get weak spots. Double-check your mold design before you mill. A small error here is a large failure later.
Rushing the Cure: Demolding too early can let the deck spring back or cause internal glue joints to fail under stress. Follow the longest recommended cure time your setup allows, especially for your first deck.
Mismatched Paint and Sealer: This creates a finish that never fully hardens or peels within weeks. It’s an easy mistake to make when you’re excited to add graphics. Read the labels on your cans.
Poor Hole Alignment: Crooked truck holes make the board pull to one side and accelerate bearing wear. The drill press is your best friend here. If you don’t have one, take extreme care and use a guide.
If you do encounter a crack or delamination, all is not lost. Our guide on how to fix a broken longboard deck covers repair techniques that can salvage your work.
How to apply grip tape to a longboard
After finishing the deck’s surface, you need to add traction for your feet. Grip tape or adhesive sandpaper is the standard solution for this. Start by ensuring the deck’s top is clean and free of dust; a tack cloth works well for this final clean-up. Carefully lay the sheet of grip tape over the deck, aligning it properly before letting it make full contact. Use a file or the edge of a screwdriver handle to rub firmly along the deck’s perimeter, creating a sharp outline. Then, cut along this outline with a sharp blade to trim the excess tape. Finally, press down firmly over the entire surface to ensure a strong bond and eliminate any air bubbles.
Frequently Asked Questions
What type of wood is best for a longboard deck?
Canadian Maple is the industry standard for its ideal strength-to-weight ratio and consistent grain. For the core of a performance deck, 0.058” maple veneers are specified. Some builders use bamboo for the outer layers to add a different flex pattern and aesthetic. The materials used in deck construction are a mix of tradition and composite science.
How do I make a homemade longboard deck without a CNC or expensive tools?
You can build a perfectly functional deck with basic tools. Create a two-part mold from hand-cut or bandsaw-cut MDF templates. Use a hydraulic bottle jack press or even a robust threaded rod press for pressure. The key is precision in your template and patience during curing. The MIT Fab Lab project used an old longboard as a one-sided mold with clamps and a vacuum bag, a great low-tech compromise.
What is the recommended thickness for a longboard deck?
There is no single answer; it depends on rider weight, desired flex, and whether you add composites like fiberglass. A pure 7-ply maple deck using 0.058” veneers will have a total thickness dependent on glue and compression. Many builders start by testing 9mm, 12mm, and 15mm plywood blanks by standing on them to gauge feel before committing to their veneer stack.
How do I attach the trucks securely?
Use a drill press to ensure perpendicular holes. The hardware (bolts, nuts, washers) must match the truck’s mounting pattern. Tighten firmly in a star pattern to distribute pressure evenly across the baseplate. For a detailed walkthrough, see our guide on how to mount longboard trucks.
Before You Go
One rule most guides skip: if you’re building for speed or aggressive riding, your deck isn’t done until it’s been stress-tested. Before you commit to a final finish, take the bare, sanded deck and flex it over your knee. Listen for cracking. Look for glue lines opening. A professional deck survives 3,200 pounds at the center; your home build needs to survive you jumping on it in your garage. That test costs nothing and reveals weaknesses the mold hid.
The first ride on a deck you made is a different kind of thrill. Every bump feedback, every carve, is a conversation with your choices in the workshop. You’ll know instantly if the flex is right, if the shape fits your stance. And if it doesn’t, you haven’t bought a lemon, you’ve learned a direct lesson for the next blank. That’s the real payoff. You’re not just assembling a board; you’re building an intuition for how deck shapes and longboard flex work underfoot. Now go break it in.